

In modern bulk material handling systems spanning mining, cement production, port logistics, power generation, and chemical processing, the conveyor belt splice is widely recognised as the weakest structural link in the entire conveying loop. Unlike the homogeneous belt body manufactured under controlled factory conditions, splices are fabricated on-site, and their performance is shaped by material compatibility, construction precision, environmental conditions, and long-term operational stress. For global industrial buyers, splice quality is no longer a secondary afterthought in procurement - it is a core determinant of system uptime, maintenance expenditure, and total cost of ownership (TCO).
Field experience across mining, cement, port and power applications points to the same conclusion: the belt splice is the most frequent single point of failure in a conveyor loop, and it is heavily over-represented among long unplanned stoppages. In heavy-duty operations, splice-related failures account for a larger share of stoppages lasting more than four hours than either cover abrasion or drive system faults taken individually. For overseas projects such as open-pit mines and bulk cargo terminals, a single 8-hour shutdown can result in US$120,000–400,000 in direct losses, including lost production revenue, vessel demurrage, emergency repair labour and secondary equipment damage.
Over the past decade, the global industrial procurement paradigm has shifted dramatically. Mature buyers no longer evaluate conveyor belts solely on price per meter; instead, they assess the full lifecycle reliability of the entire system, including splice materials, technical support, and maintenance services. This guide breaks down core vulcanization mechanisms, identifies the main failure drivers, and outlines standard O&M protocols drawn from field experience. It aims to help procurement teams identify high-value suppliers, avoid common cross-border sourcing pitfalls, and optimize long-term operational costs through informed decision-making.
Performance Benchmark: Comparison of Mainstream Splicing Technologies
Three splicing technologies dominate industrial applications worldwide: hot vulcanized splicing, cold bonded splicing, and mechanical fastener splicing. The three rest on different physical and chemical principles and differ widely in strength retention, service life, installation time, upfront cost and long-term maintenance requirement. There is no single best solution; for any given duty, however, one option will deliver the lowest total cost of ownership.
Hot vulcanized splicing works by applying controlled heat and pressure to uncured rubber compounds at the splice interface, triggering a cross-linking reaction that merges the splice material with the original belt body into a unified structure. It is the only method that restores a high proportion of the original belt's tensile strength - typically 85–96%, depending on carcass type. Cold bonding relies on room-temperature chemical adhesives to bond the cut belt ends, requiring no heating equipment but delivering lower strength and poorer long-term aging resistance. Mechanical fastening uses metal or plastic clips to physically clamp the two belt ends together, offering the fastest installation but the lowest strength and shortest service life.
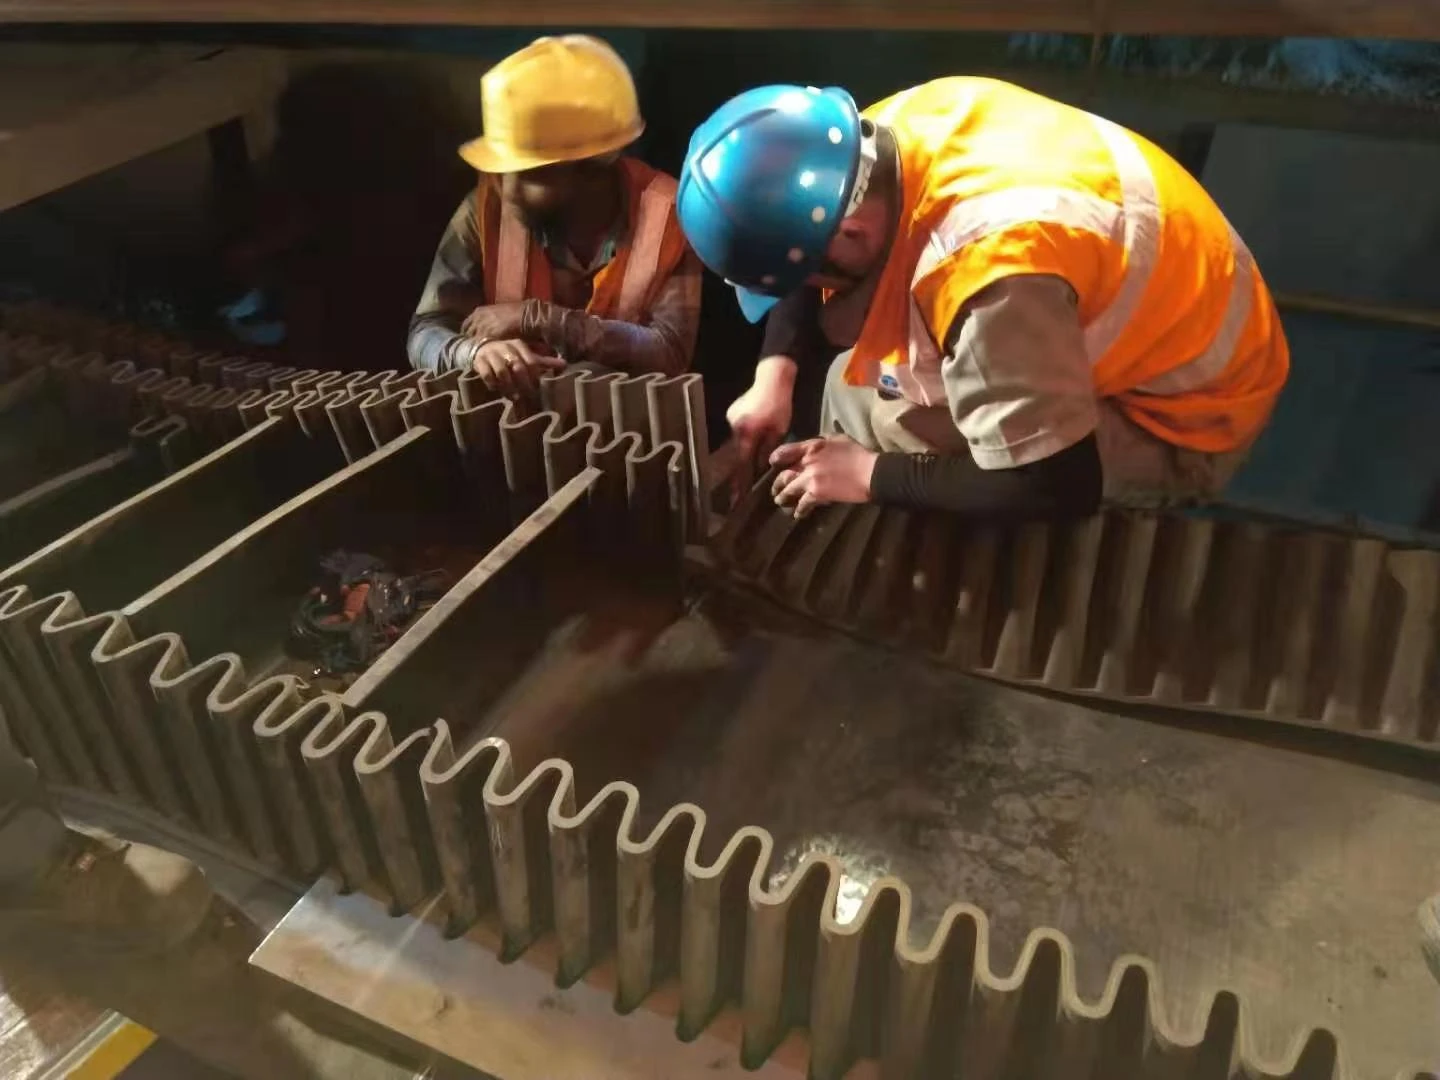
Table 1: Comprehensive Performance Comparison of Conveyor Belt Splicing Methods
|
Splicing Method |
Strength Retention Rate (vs. original belt) |
Average Service Life |
Typical Installation Downtime |
Initial Cost Index (base: mechanical = 1.0) |
Recommended Applications |
|
Hot Vulcanized Splice |
Fabric ply belts: 85–92% Steel cord belts: 90–96% Typical values for correctly executed splices, confirmed by splice tensile test |
3–8 years (matches belt body lifespan under proper O&M) |
4–8 hours (full cycle: heating → curing → cooling) |
2.5–3.5 |
Heavy-duty long-haul main lines, high-tension conveyors, continuous 24/7 operation, underground mining, high-abrasion loading zones |
|
Cold Bonded Splice |
75–85% |
1–3 years |
2–4 hours application + 4–8 hours static curing |
1.5–2.0 |
Medium-light duty lines, indoor facilities with no hot work permits, explosion-hazard chemical plants, short-distance assembly lines |
|
Mechanical Fastener Splice |
40–60% |
6–18 months |
0.5–2 hours |
1.0 |
Temporary emergency repairs, short low-tension belts, seasonal operations requiring frequent belt disassembly, light-duty packaging lines |
Data source: representative manufacturer test data and field experience from mining, cement and port operations. Strength retention figures are typical values for correctly executed splices and should be confirmed by splice tensile testing to ISO 15236-4 (steel cord belts) or the applicable textile-belt splice specification. Cost indices are relative estimates, not quoted prices.
For high-tension steel cord belts used in long-distance overland conveyors and high-capacity mine haulage systems, hot vulcanization is the only technically accepted solution. Many procurement teams underestimate the hidden cost of mechanical fasteners: the material itself is inexpensive, but the fasteners create severe stress concentration at each joint, accelerate pulley and idler wear, cause persistent material leakage, and require re-tightening or replacement every few months. In 24/7 heavy-duty operation, field experience shows that mechanical fasteners can drive annual maintenance cost to several times that of a properly executed vulcanized splice, while sharply increasing the risk of sudden catastrophic breakage.
Cold bonding is a viable compromise for medium-duty indoor lines where hot work is prohibited by safety regulations, but it is highly sensitive to on-site temperature, humidity and surface cleanliness. In high-humidity tropical regions or dusty industrial environments, cold bond splice failure rates can be more than double those achieved under controlled indoor conditions, which makes hot vulcanization the more reliable choice despite the longer installation time.
Critical Process Parameters for Qualified Hot Vulcanized Splicing
The strength and durability of a vulcanized splice are not determined by the press equipment alone, but by the precise control of every process parameter throughout the entire construction workflow. Vulcanization is essentially an irreversible chemical cross-linking reaction of rubber polymers: under specific temperature and pressure, sulfur and other curing agents form three-dimensional molecular bonds between rubber chains, transforming soft, plastic uncured rubber into a strong, elastic, wear-resistant cured structure. Even small deviations from the optimal parameter range can cause irreversible performance degradation.
The table below summarises widely used industry reference values for core vulcanization parameters, with differentiated specifications for fabric ply and steel cord belts according to their structural characteristics and stress modes. The cure chart issued for the specific belt compound always takes precedence over generic values.
Table 2: Standard Hot Vulcanization Process Parameters by Belt Type
|
Process Parameter |
Fabric Ply Belts (EP/NN) |
Steel Cord Belts (ST) |
Consequence of Out-of-Range Value |
|
Curing Temperature |
145–155°C (optimal: 150°C) |
145–155°C (optimal: 150°C) |
Under-curing (<140 °C): incomplete cross-linking; adhesion falls below 60% of rated value and the splice delaminates early under cyclic load. Over-curing (>160 °C): polymer chain degradation and rubber embrittlement; dynamic fatigue life reduced by 50% or more, with cracking under repeated bending. |
|
Curing Pressure |
1.5–2.0 MPa |
2.0–2.5 MPa |
Insufficient pressure: internal voids and inter-layer delamination; voids above 0.5 mm cut dynamic fatigue life by around 40%. Excessive pressure: rubber squeezed out, uneven ply thickness and local stress concentration, lower fatigue resistance. |
|
Constant-Temperature Curing Time |
1.5–2 min per mm of total belt thickness |
2–2.5 min per mm of total belt thickness |
Shortened cure: inadequate cross-link density; peel strength 30% or more below specification, with early delamination under cyclic load. |
|
Bonding Surface Preparation |
Uniformly roughened, matte, dry, lint-free |
Uniformly roughened, matte, dry, lint-free |
Too smooth or glazed: insufficient mechanical keying; bond strength up to 25% below specification. Too rough or contaminated: damaged ply fibres or cord coating, entrapped air, early fatigue cracking. |
|
Minimum Lap / Embedment Length |
150–300 mm per ply (varies by strength grade) |
Stepped splice per ISO 15236-4: transition length 100–250 mm by cord diameter (minimum 16 × d) |
Insufficient length: tensile rupture at the splice under rated operating load. |
Data source: consolidated manufacturer cure specifications and field splicing records. The parameter windows are reference values; the cure chart issued for the specific belt compound always takes precedence.
Beyond the core curing parameters, on-site construction practice has an equally significant effect on final splice quality. All bonding surfaces must be cleaned of release agents, dust and grease, and freed from moisture before rubber cement is applied; the cement should then be applied in uniform thin coats, with adequate drying time between coats. For steel cord belts, individual cords must be laid out in a staggered diamond pattern so that stress is distributed evenly across the full belt width and no single row of cords carries a concentrated load.
Environmental conditions during construction cannot be ignored either. Ambient temperature on site should stay above 5 °C throughout the process. Work below 0 °C requires preheating and insulation to prevent slow cure and moisture condensation at the bond interface. At altitudes above 3,000 m, lower atmospheric pressure reduces the boiling point of water and slows heat transfer, so curing time must be extended by 15–30% to compensate. Rushing the cooling phase is another common mistake: the splice must be cooled below 60 °C while still under pressure before the press is opened; releasing pressure early causes thermal stress deformation and permanent internal damage.
Standardized O&M Framework: Extending Splice Lifespan and Reducing Downtime
Systematic inspection and preventive maintenance are the most cost-effective ways to protect the splice investment. Field experience shows that a disciplined O&M routine can extend average splice service life by around 30% and greatly reduce the risk of sudden catastrophic failure. For overseas projects with limited on-site technical resources and long spare-part lead times, a tiered inspection regime is essential to avoid costly unplanned shutdowns.
The following tiered inspection schedule is widely adopted by leading mining and logistics operators worldwide, differentiated by line criticality so that maintenance resources go where they matter most.
Table 3: Tiered Inspection Schedule for Vulcanized Belt Splices
|
Inspection Tier |
Frequency (Heavy-Duty Main Line) |
Frequency (General Industrial Line) |
Inspection Method |
Key Check Items & Acceptance Criteria |
|
Routine Visual Inspection |
Weekly |
Bi-weekly |
Visual check + handheld thickness gauge |
1. No edge cracks longer than 20 mm. 2. No surface bulges, blisters or edge delamination. 3. Remaining cover thickness ≥ 50% of original specification. |
|
Detailed Operational Check |
Monthly |
Quarterly |
Run-to-stop observation + infrared temperature gun |
1. No abnormal temperature rise at the splice (ΔT ≤ 5 °C against adjacent belt). 2. No abnormal vibration or impact noise when passing pulleys. 3. No material leakage or uneven belt tracking at the splice. |
|
Non-Destructive Testing (NDT) |
Annually |
Every 2 years |
Ultrasonic testing / X-ray inspection (for steel cord belts) |
1. No internal voids larger than 0.5 mm. 2. No cord displacement, breakage or corrosion. 3. No inter-layer delamination at bond interfaces. |
Data source: operator inspection standards from mining and bulk terminal practice, aligned with the joint documentation requirements of ISO 15236-4. Frequencies should be shortened where belt speed, tonnage or material abrasiveness exceeds the design basis.
Beyond regular inspection, targeted preventive maintenance measures address the root causes of splice degradation outlined above. For outdoor or high-humidity locations, applying polyurethane edge sealant to splice edges creates an impermeable barrier that blocks moisture and corrosive media intrusion, extending splice life by 20–30% in coastal and tropical environments. Loading zone optimization - including installation of impact beds, properly adjusted chute skirts and material flow guides - reduces impact force and abrasive wear on splices and belt bodies alike.
Regular alignment calibration is another high-return maintenance practice. Pulley and idler alignment should be performed every 6 months using laser alignment tools, controlling belt running deviation within 1% of belt width. That one measure removes the largest single cause of splice edge failure and also reduces idler and pulley wear across the entire system.
For large fleets of conveyors, implementing lifecycle traceability management delivers significant operational value. Each splice should be assigned a unique ID, with records of installation date, vulcanization parameters, technician name, batch numbers of materials used, and full history of inspection results and repairs. This record supports predictive maintenance planning, enables root-cause analysis when a failure occurs, and helps optimize future procurement specifications based on actual field performance.
Procurement Value Proposition: Integrated Splice Solutions for Global Buyers
For global industrial buyers, the most reliable and cost-effective way to control splice risk is to source both the belt body and the matching splice consumables from the same manufacturer. That single decision secures formulation compatibility, consistent performance around the entire belt loop, and one point of accountability when something goes wrong. The four criteria below are the ones we would apply when evaluating any integrated belt-and-splice supplier; we set out our own practice against each of them.
1.Formulation-Matched Splice Kits for Guaranteed Compatibility
Every grade of our conveyor belt is paired with dedicated core rubber, cover rubber and rubber cement produced from the same polymer formulation and curing system as the belt body. That consistency maximises interfacial cross-linking during vulcanization and keeps splice and belt aging at the same rate. Our splices achieve strength retention at the upper end of the ranges quoted in Table 1 - typically 90–92% for fabric ply belts and 94–96% for steel cord belts - confirmed by third-party laboratory testing. Because the compound system matches, there is no interfacial compatibility risk, and performance stays predictable over the long term even in harsh duty.
2.Specialty Compounds for Extreme Duty
For heat-resistant, flame-retardant, oil-resistant, cold-resistant and other special-purpose belts, we supply splice compounds that match the belt compound itself. Our heat-resistant splice compounds are EPDM-based to suit T1–T4 grade belts, retaining bond strength at continuous service temperatures of 120–150 °C (T3–T4) with short-term peaks up to 200 °C. Our underground mining kits meet ISO 340 flame-retardant and ISO 284 antistatic requirements, and comply with MSHA flame-resistance approval requirements and EN 14973. Matching the compound is what keeps the splice from becoming the weak point in special-duty applications - the usual outcome when general-purpose splice material is used on a specialty belt.
3.Complete Technical Support for Overseas Projects
Every export shipment includes an English-language vulcanization procedure manual, parameter tables customised to the specific belt specification, and step-by-step construction guidelines with illustrations. Our technical team provides remote support for overseas projects, with real-time troubleshooting during splicing. For large projects we can arrange on-site supervision and operator training so that the site crew executes the work exactly to factory specification. We also advise on inspection protocols, preventive maintenance and splice lifecycle management, helping clients build in-house maintenance capability.
4.Full Traceability and Quality Assurance
All our splice kits carry unique traceable batch numbers, full raw material records and third-party test reports, and comply with the applicable ISO, ASTM and DIN standards. Complete production records are kept for every batch, so any quality question can be traced back through the chain. For clients with strict procurement compliance requirements, we support pre-shipment inspection by third parties such as SGS and BV, giving independent verification of material quality and performance.
Choosing an integrated belt-and-splice solution removes the two risks that most often derail cross-border procurement: material mismatch and inconsistent quality between suppliers. Customers who make the switch typically report a 15–20% reduction in the maintenance and downtime component of conveyor TCO, achieved through longer splice life, fewer unplanned shutdowns, lower labour cost and simpler procurement. We work with each client to optimise splice design and O&M protocols for their actual operating conditions.
If you need reliable vulcanized splice kits, please contact us. We can provide professional technical support, matched splice compounds, full test certificates and customized splicing solutions to meet your actual on-site operating requirements.
Email: sunny@bestfriendrubber.com
WhatsApp / Tel: +86 139 6972 9233
Inquiry form: https://www.qbfrubber.com/inquiry
FAQ
Q: Which splicing method should I choose - hot vulcanized, cold bonded or mechanical?
A: Hot vulcanization is the only method that restores 85–96% of original belt strength and the only technically accepted option for high-tension steel cord belts. Cold bonding suits medium-duty indoor lines where hot work is prohibited; mechanical fasteners install fastest but cost far more in maintenance and breakage risk.
Q: How much strength does a vulcanized splice retain?
A: Typically 85–96% of the original belt, depending on carcass type - fabric ply at the lower end, steel cord at the upper end. Confirm it by splice tensile testing to ISO 15236-4 before accepting the joint.
Q: Why do most splices fail before their design life?
A: Well over half of premature failures come from system design, material mismatch and neglected O&M rather than poor workmanship. The main drivers are pulley misalignment, non-matching splice compounds, impact loading at chutes, moisture ingress, and incorrect tension or aggressive belt cleaners.
Q: How often should splices be inspected, and what tolerance should alignment hold?
A: Use a tiered schedule based on line criticality, shortening intervals where speed, tonnage or abrasiveness exceeds the design basis. Check pulley and idler alignment every six months with laser tools and keep belt run-out within 1% of belt width - a disciplined routine typically extends splice life by about 30%.


